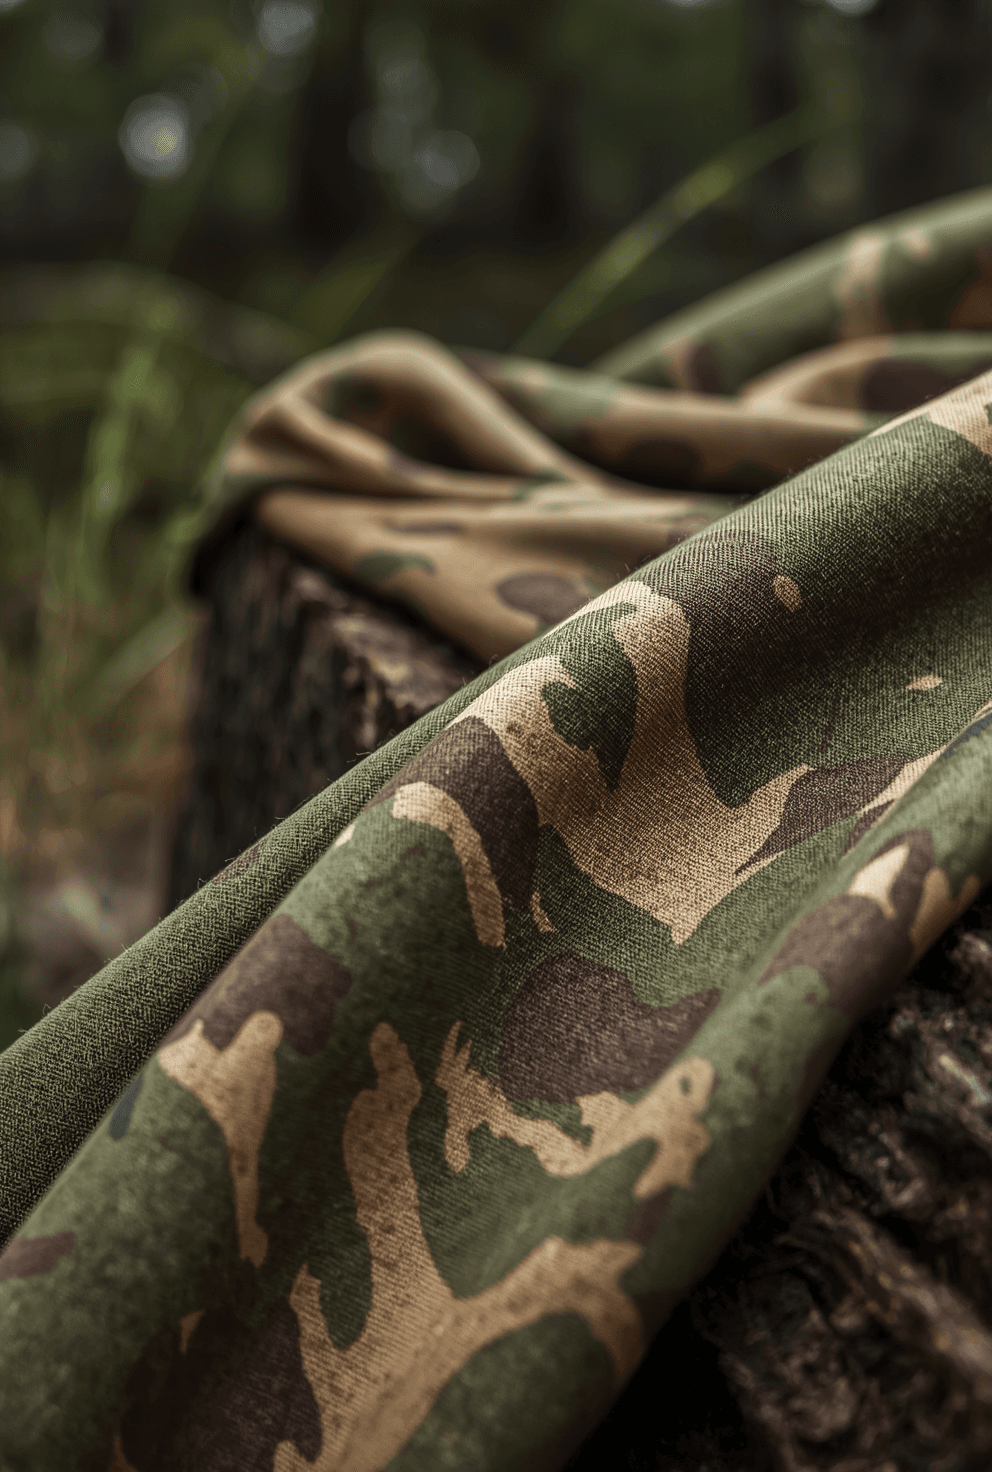
Tactical and Military
Extreme durability and mission-ready protection for demanding tactical gear.
Vertically Integrated Fabric Partner
Engineering what others can't. A vertically integrated partner delivering high-difficulty custom fabrics for brands that demand the absolute best.

Purpose-built fabric systems for tactical, workwear, golf, medical, lingerie, and outdoor categories with scalable manufacturing logic.
Extreme durability and mission-ready protection for demanding tactical gear.
Industrial-grade durability combined with daily wearing comfort and safety.
Premium hand-feel with dynamic moisture management and antibacterial performance.
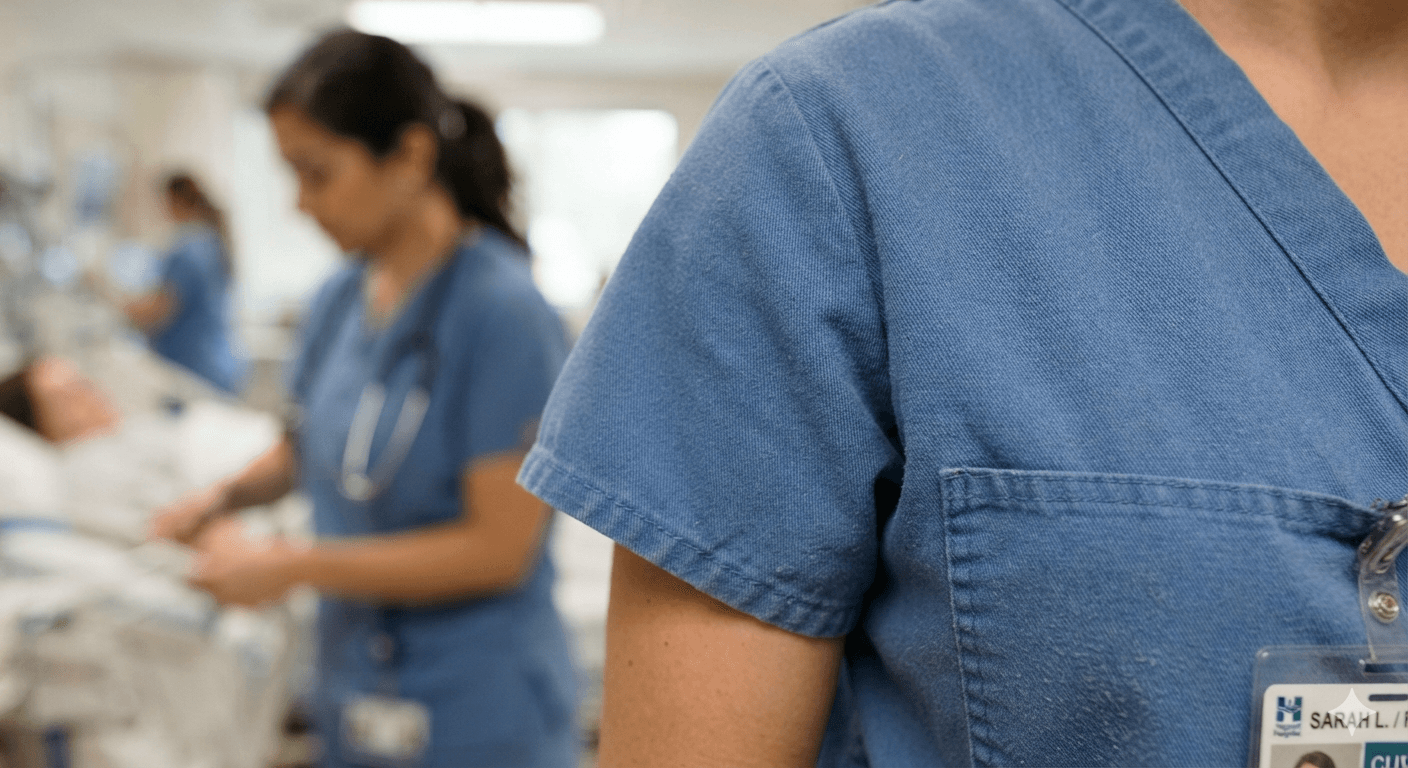
Antibacterial and fluid-resistant barrier fabrics designed for healthcare safety.
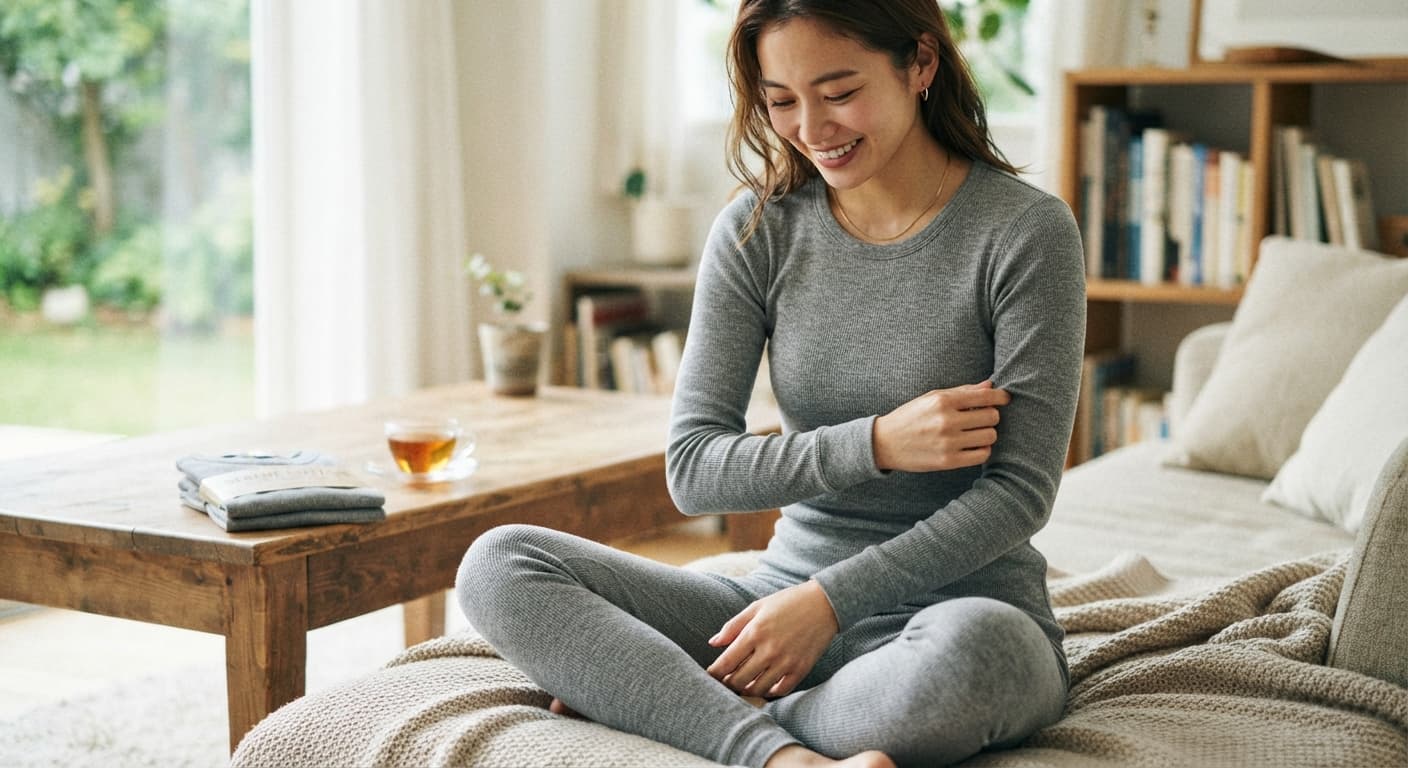
Ultra-soft, breathable, and antibacterial fabrics for next-to-skin comfort.
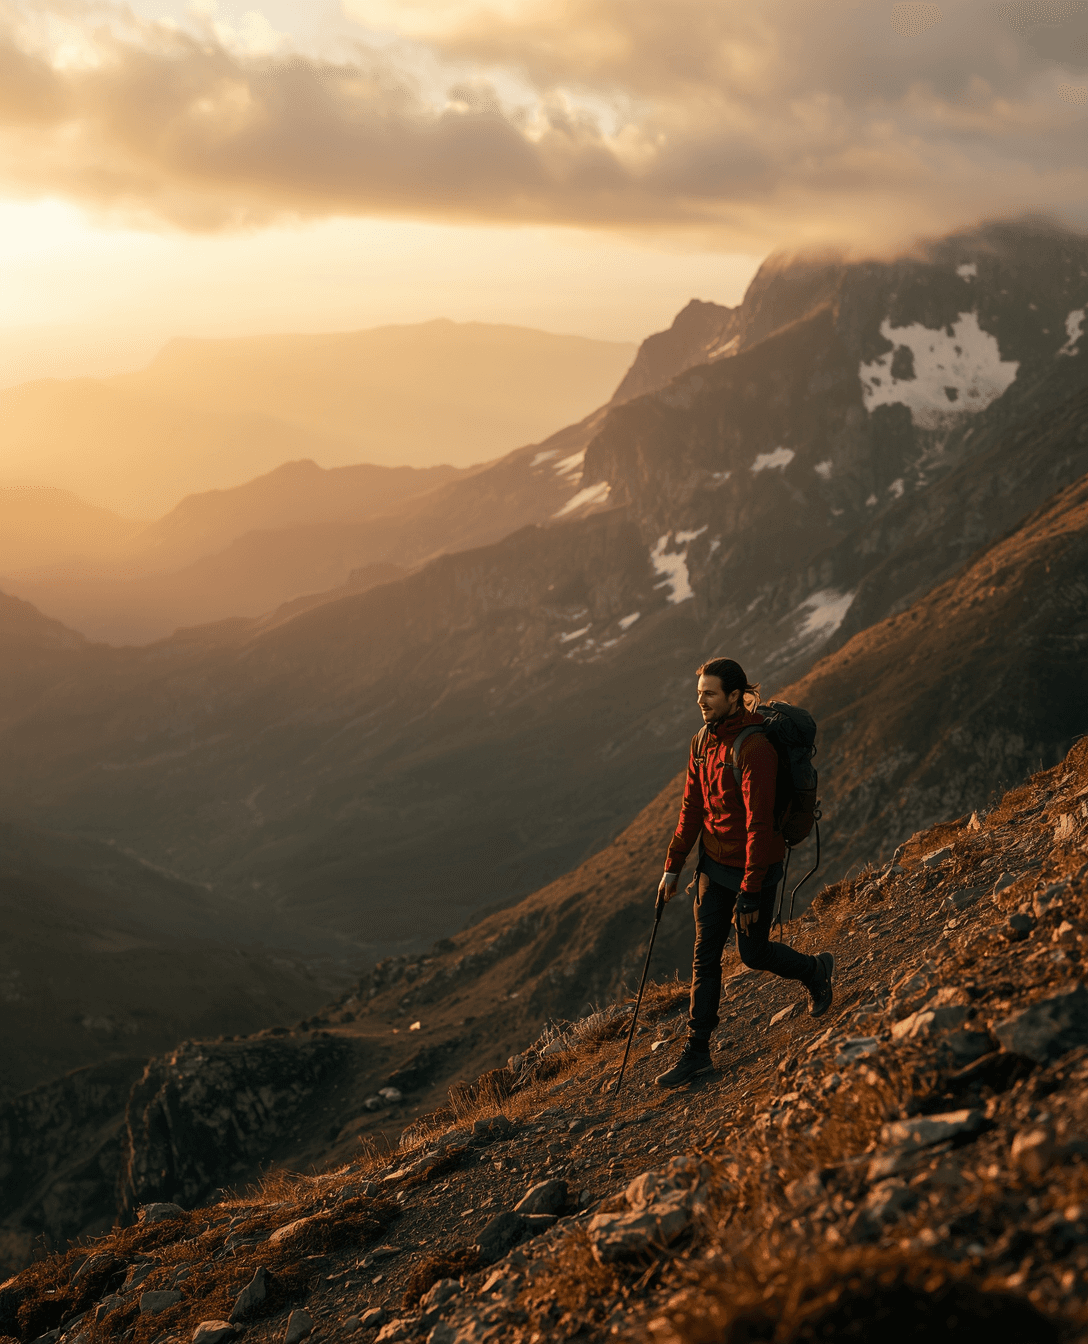
Phase-change temperature regulation and weather protection for active performance.
Infusing medical-grade high-purity Zinc Oxide directly into fiber strands, delivering permanent natural antibacterial, anti-mold, superior UV protection (UPF 50+), and hypoallergenic skin comfort. Our flagship core technology.
Permanent Antibacterial
Wash-durable protection
UPF 50+ UV Shield
Maximum sun protection
Medical-Grade ZnO
Infused directly in yarn
Hypoallergenic Comfort
Ideal for next-to-skin wear
Selecting premium natural and synthetic fibers to build the optimal foundation for physical performance and next-to-skin comfort.
Lyocell
Lyocell
Tencel
Tencel
Nylon
Nylon
Polyester
Polyester
Cotton
Cotton
Wool
Wool
Rayon
Rayon
CVC
CVC
TC
TC
Spandex
Spandex
We manage the entire textile supply chain from yarn R&D, weaving, and dyeing to functional finishing and final inspection.
Custom blending of functional fibers to establish core fabric properties.
Selecting precise knit or woven structures to optimize weight, density, and physical tear strength.
Advanced shade matching and color fastness treatment to ensure repeatability across production batches.
Applying performance coatings, laminations, and treatments like antibacterial, PCM, or water repellency.
Strict point-system inspection and lab testing before packaging to ensure zero-defect delivery.
Translating brand design concepts into high-performance fabrics through rigorous process control and functional R&D.
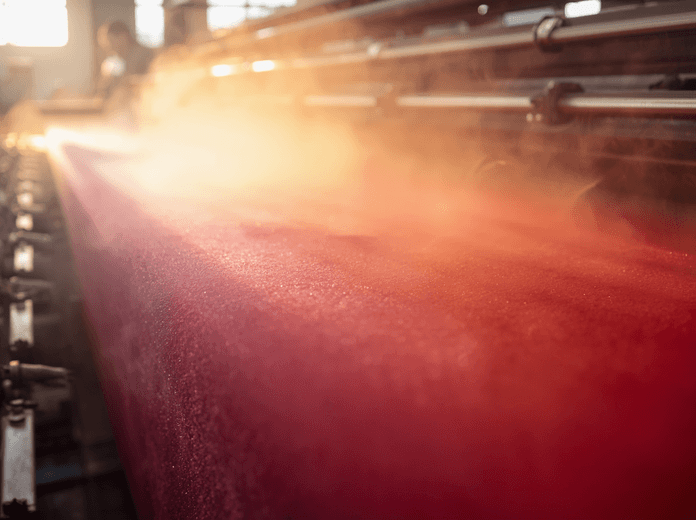
From shade precision to hand-feel control, we tune process parameters for repeatable production results.
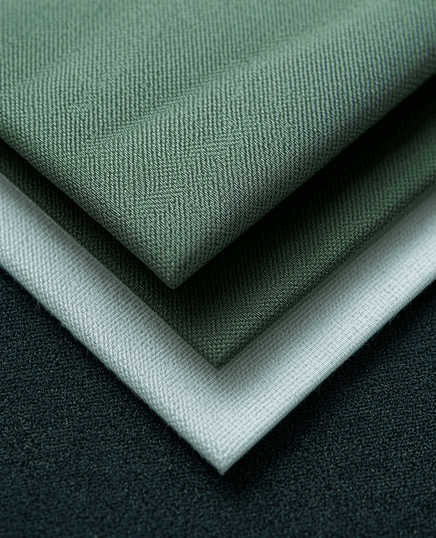
Build balanced structures for waterproofing, breathability, and protection under demanding conditions.
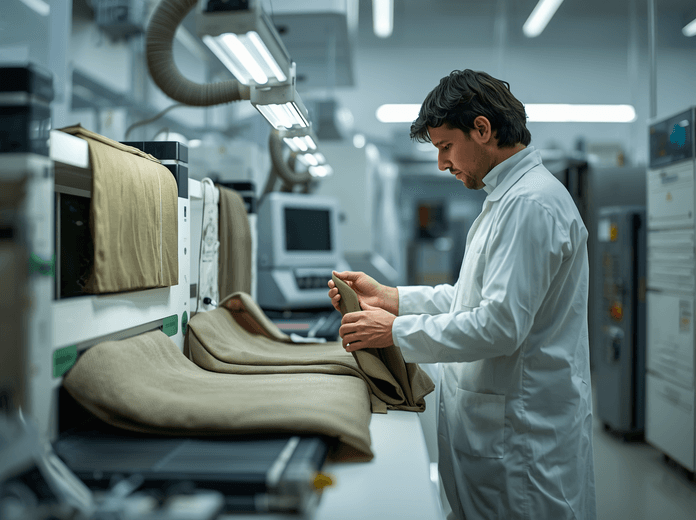
Structured checkpoints from development to mass production reduce risk and accelerate launch timelines.
Infusing advanced textile technologies to deliver antimicrobial, thermal regulation, heat retention, and superior moisture management.
Incorporating medical-grade zinc oxide into yarn, delivering natural permanent antibacterial protection, UPF 50+ UV blocking, and hypoallergenic skin-soothing comfort — our signature technology.
Long-lasting inhibition of bacterial growth, preventing odor and mold, ideal for next-to-skin and medical use.
Special fiber cross-sections pull moisture away from the skin rapidly, ensuring dry comfort.
Effective UV blocking (UPF 50+) to protect skin during outdoor activities and high-sun exposure environments.
Infused with mineral microparticles to reflect body heat, promoting microcirculation and warm retention.
Dynamically regulates skin microclimate by absorbing and releasing heat, maintaining thermal comfort.
Compliant with international flame retardant standards, inhibiting fire spread for safety in high-risk work environments.
Surface-raising, sueding, and fleece finishing processes deliver unique hand-feel textures and enhanced warmth.
Specialty crinkle and print processing delivers rich visual texture and fashion-forward aesthetics for diverse design needs.

01
Confirm application scenario, target performance, and timeline with your product team.

02
Propose suitable constructions, finishing options, and functional layer combinations.

03
Run lab and wear-performance checks to verify quality consistency and specification fit.

04
Transition to production with process controls, quality checkpoints, and delivery visibility.
We partner with certified production ecosystems and prioritize responsible sourcing to support brand-level environmental goals.
Our development path emphasizes traceability, safe chemistry alignment, and practical implementation at production scale.
GRS Aligned
OEKO-TEX
Delivering bespoke high-performance fabric solutions for leading brands across various industries.
Engineered ultra-durable, flame-retardant nylon blends with NIR compliance, meeting stringent field mission requirements.
Developed high-tenacity canvas fabric withstanding 50+ industrial washes while maintaining oil and water repellency.
Created a soft-drape knit fabric combining permanent antibacterial treatment with superior four-way stretch comfort.
Designed fluid-resistant, breathable barrier fabrics capable of withstanding high-temperature autoclave sterilization.
Formulated an ultra-fine Lyocell-Spandex blend with natural botanical antibacterial properties and silk-like touch.
Integrated phase-change temperature regulating layers with PFC-free DWR coatings for dynamic climate adaptation.

Certified manufacturing partners across regions supporting global brand expansion.

Rapid technical response within 48 hours to address development challenges.

Traceable quality checkpoints from sampling to mass production.
Yes. We specialize in custom R&D based on target performance, hand-feel, end-use conditions, and manufacturing feasibility. We welcome challenging specifications.
Our manufacturing partners are fully aligned with GRS and OEKO-TEX Standard 100 to support environmental and safety requirements.
Yes. We collaborate with international brands across tactical, workwear, golf, medical, lingerie, and outdoor categories.